Choosing the China Best Fiberglass Profile Supplier for Global Buyers requires more than comparing prices. A reliable Fiberglass Profile partner should combine manufacturing experience, technical knowledge, quality control, and consistent communication. The right supplier understands how profiles perform in construction, electrical insulation, transportation, and industrial environments. They should also explain material choices clearly, including glass fiber content, resin systems, surface finishes, and dimensional tolerances.
Production details matter. A professional factory can show how pultrusion lines are operated and maintained. Engineers should discuss tensile strength, bending performance, water absorption, UV resistance, and fire requirements. Depending on the application, buyers may request testing against ASTM, EN, ISO, or other relevant standards. Inspection records, batch numbers, material certificates, and traceability documents can reveal whether quality is controlled or simply promised. Small details matter.
Yet “best” is not universal. A supplier with advanced equipment may still provide weak technical support. Another factory may offer excellent profiles but lack efficient export experience. This is where careful verification becomes necessary. Buyers should review samples, inspect packaging, confirm lead times, and speak with existing customers when possible. A factory audit can expose practical issues, such as uneven resin distribution or poor storage conditions. These problems are easy to overlook in polished presentations.
Experience teaches a useful lesson: low price rarely describes total value. Freight damage, inconsistent dimensions, and delayed documentation can increase project costs. A dependable supplier offers clear specifications, responsive communication, and realistic commitments. The evaluation should remain open-minded. No manufacturer is perfect, and every project deserves a fresh technical review before a long-term decision.
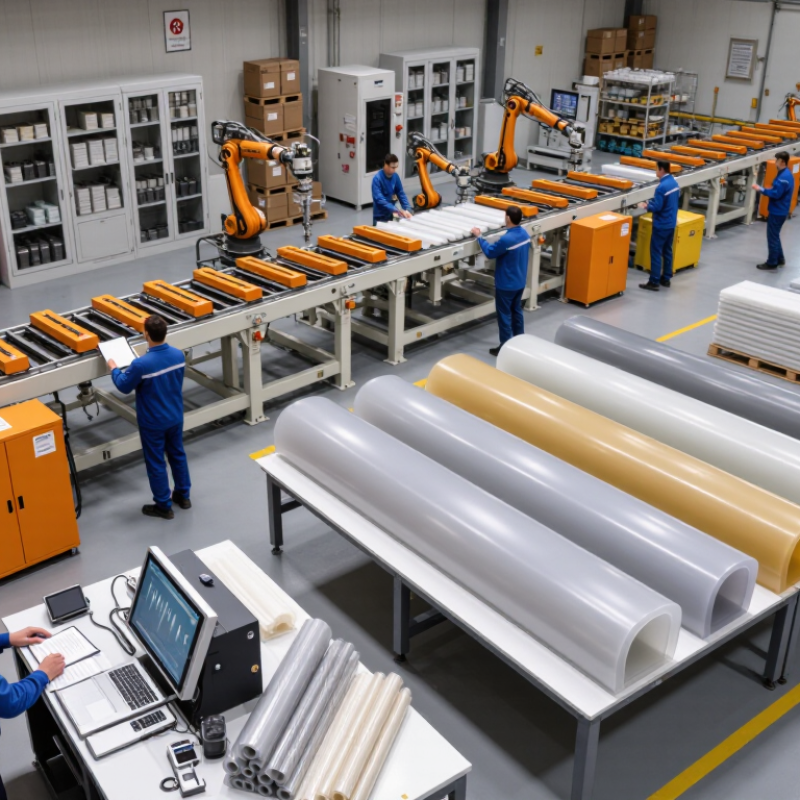
Fiberglass profiles are structural shapes made from glass fibers and a polymer resin. They combine low weight with useful strength, corrosion resistance, and electrical insulation. Unlike steel, fiberglass does not rust in wet industrial environments. It also offers stable performance around many chemicals, although resin selection remains critical.
Common types include solid rods, flat bars, angles, channels, tubes, grating, and custom sections. Each profile serves a different purpose. Tubes can support lightweight frames, while pultruded grating suits platforms and walkways.
Surface options also matter. A smooth finish supports clean handling, but a grit surface improves slip resistance. Small details affect safety.
Pultrusion is a continuous manufacturing process. Glass rovings, mats, or fabrics pass through a resin bath. Then, guides arrange the reinforcement before a heated die shapes and cures the profile. Pulling equipment maintains a steady speed. Cutting follows the required length. In real production, tension, resin temperature, and die alignment need constant attention. Minor errors can create uneven walls or weak corners.
For global buyers, supplier evaluation should include fiber content, resin data, dimensional tolerances, and test records. Samples should be checked for straightness, surface defects, and fit. A perfect appearance proves little. I have seen profiles look excellent while showing inconsistent bonding inside. That is why independent testing and traceable production records remain valuable, even when delivery pressure is high.
China remains the largest manufacturing base for fiberglass profiles, supported by broad glass-fiber yarn, resin, pultrusion, and machining capacity. Industry association statistics commonly place China’s share of global glass-fiber output above 70%. This concentration supports flexible order volumes, but capacity does not always equal consistent quality.
MarketsandMarkets estimates that the global glass-fiber market will grow from about USD 15.7 billion in 2023 to USD 20.3 billion by 2028, at a 5.3% CAGR. Construction, transportation, electrical insulation, and corrosion-resistant infrastructure drive demand. For buyers, this growth means more suppliers, but also wider differences in profile tolerances, resin systems, and testing records.
A practical supplier assessment should examine production lines, annual output, and batch traceability. It should also verify tensile strength, flexural strength, glass content, and dimensional stability through independent testing. China’s supply network can support custom colors, drilled sections, and continuous lengths. However, published capacity figures may include theoretical production, not available monthly capacity. That detail is easy to miss. Buyers should request recent inspection reports, sample approvals, and realistic lead times before signing long-term contracts. Industry forecasts are helpful, but they cannot replace factory-level evidence.
For global buyers, fiberglass profiles should be judged by measured performance, not polished catalog language. A glass fiber content of 60–75% usually indicates a load-focused pultruded structure. More reinforcement can improve stiffness, dimensional stability, and resistance to long-term bending. It can also make processing less forgiving. Resin distribution matters. Voids, uneven wet-out, or poor curing may weaken an otherwise impressive profile. In factory audits, inspect cut sections and review batch records.
A reported strength of 3,400 MPa requires careful interpretation. If this figure describes the glass fiber, it should not represent the finished profile’s strength. The composite value is typically lower and depends on fiber direction, resin chemistry, curing quality, and test conditions. Ask whether the result measures tensile, flexural, or compressive strength. Request the testing standard, specimen shape, temperature, and failure location. Direction matters greatly.
Small details reveal supplier reliability. Check profile straightness, surface cracks, fiber exposure, and dimensional tolerances across several production lots. Samples should match mass production, not receive special treatment. That sounds obvious. It is often missed. A technically strong profile may still fail in service when drilling, joining, or exposing it to moisture. Confirm connection methods and aging data before approving a large order. Independent laboratory verification adds useful confidence, although it cannot replace process control. The best purchasing decision combines the 60–75% reinforcement target with transparent evidence for actual profile performance.
| Technical Metric | Typical Reference Value | Common Test Method or Standard | Technical Relevance for Global Buyers |
|---|---|---|---|
| Glass Fiber Content by Mass | 60–75% | ASTM D2584 or thermogravimetric analysis | A typical range for structural pultruded glass-fiber-reinforced polymer profiles. Higher fiber content generally improves longitudinal stiffness and strength, provided wet-out and consolidation are properly controlled. |
| Glass Fiber Type | E-glass, continuous or roving reinforcement | Material declaration and compositional verification | E-glass is widely used because it provides a practical balance of tensile strength, electrical insulation, corrosion resistance, and cost. |
| Bare E-Glass Filament Tensile Strength | Approximately 3,400–3,500 MPa | ASTM D2343 or ISO 11566 | This value applies to the glass filament, not directly to the finished composite profile. The final profile strength is lower and depends on fiber alignment, resin system, void content, geometry, and processing. |
| Pultruded Profile Longitudinal Tensile Strength | Approximately 300–1,000 MPa | ASTM D638, ASTM D3917, or ISO 527 | The actual result varies significantly with fiber architecture, resin chemistry, profile shape, test direction, specimen preparation, and manufacturer quality controls. |
| Longitudinal Tensile Modulus | Approximately 25–50 GPa | ASTM D638, ASTM D3917, or ISO 527 | A key design value for beams, ladders, gratings, frames, and structural channels where deflection control is important. |
| Flexural Strength | Approximately 300–900 MPa | ASTM D790 or ISO 14125 | Useful for evaluating bending performance. Results depend on laminate construction, support span, specimen dimensions, and whether the profile is solid, hollow, or shaped. |
| Flexural Modulus | Approximately 20–45 GPa | ASTM D790 or ISO 14125 | Supports preliminary calculations for bending stiffness and serviceability. Final structural calculations should use certified product-specific data. |
| Density | Approximately 1.8–2.0 g/cm³ | ASTM D792 or ISO 1183 | Typically lower than steel, which can reduce handling and installation weight while retaining useful structural performance. |
| Water Absorption | Usually below 1.0% by mass after conditioning | ASTM D570 or ISO 62 | Low water absorption helps maintain dimensional stability and mechanical performance in humid or wet environments. The result depends on resin, surface finish, and void content. |
| Continuous Service Temperature | Approximately 65–120°C | Resin technical data and heat-deflection testing | The applicable limit is governed mainly by the resin system, glass-transition temperature, loading conditions, and exposure time. A project-specific temperature rating is required. |
| Coefficient of Thermal Expansion | Approximately 5–15 × 10−6/°C longitudinally | ASTM E831 or ISO 11359 | The longitudinal value is generally lower than that of the transverse direction because of aligned glass fibers. This matters for long profiles and assemblies exposed to temperature changes. |
| Electrical Insulation | Non-conductive when produced with insulating resin and without conductive fillers | ASTM D149, ASTM D257, or IEC 60093 | Suitable for many electrical-access and utility applications, but insulation performance must be verified for the specific resin, moisture condition, thickness, and voltage environment. |
| Corrosion Resistance | High resistance to moisture, salts, and many industrial chemicals | ASTM G20, ASTM B117, or project-specific chemical exposure testing | Chemical compatibility depends on resin formulation, concentration, temperature, exposure duration, and mechanical loading. A chemical-resistance confirmation should be obtained for demanding environments. |
| Dimensional Tolerance | Defined by profile geometry and applicable pultrusion specification | ASTM D3917 or approved production drawings | Buyers should specify critical dimensions, straightness, twist, wall thickness, cut length, surface finish, and inspection frequency before production approval. |
| Quality Documentation | Material certificate, inspection report, batch traceability, and test results | ISO 9001-based quality system and purchase specification | For international procurement, documentation should identify the product specification, test direction, specimen size, conditioning, batch number, and acceptance criteria. |
Choosing a fiberglass profile supplier requires more than comparing quotations. A valid ISO 9001 certificate shows a controlled management system, not automatic product quality. Check its scope, issue date, certification body, and factory location. Ask whether the certificate covers pultrusion, inspection, and shipment processes.
ASTM and EN references should match your application. Request the exact standard numbers, test methods, acceptance limits, and latest laboratory reports. Do not accept “ASTM compliant” without details. Paper is not proof. A reliable supplier can provide production samples, dimensional records, resin information, fiber content, and mechanical test results. Independent testing adds useful confidence, especially for structural profiles.
Quality control should be visible on the factory floor. Look for incoming checks on glass fiber and resin, controlled pulling speed, temperature records, surface inspections, and batch traceability. Profiles should be measured for width, thickness, straightness, color, and drilling accuracy. Ask how nonconforming products are isolated and corrected. A serious supplier will explain corrective actions without hiding weak points.
Small details matter. Check packaging, moisture protection, labeling, and loading photos. A remote audit helps, but it cannot replace every physical inspection. Sample approval may also mislead if production controls change later. Keep this limitation in mind. Clear drawings, signed specifications, retained samples, and agreed inspection points make supplier performance easier to verify.
Export, Customization, and Compliance Factors for Global Buyers
Selecting a fiberglass profile supplier involves more than comparing prices. Export experience matters when profiles must travel across climates, ports, and handling conditions. Experienced suppliers confirm dimensions, resin type, glass content, surface finish, and packaging before production. A 6-meter profile may need reinforced cartons, moisture barriers, and clear loading instructions. Small packing mistakes can cause damage.
Customization should be practical, not decorative. Buyers may request drilled holes, pultruded channels, colored surfaces, or tighter tolerances. The supplier should provide drawings, samples, and measurable inspection standards. Test reports should explain tensile strength, flexural performance, water absorption, and flame behavior. Ask how often testing occurs. One report may not represent every production batch.
Compliance requires destination-specific attention. Documentation may include material declarations, safety data, factory inspection records, and certificates accepted by the importing market. Customs descriptions and HS codes must match the actual product. This detail is often underestimated. A capable export team checks labeling, pallet dimensions, and required documents before shipment. Yet no supplier gets every project right. Specifications can change late, and test methods may be misunderstood. Honest communication, traceable revisions, and corrective action are more reliable than confident promises. Get everything in writing.
Copyright © 2025 · All Rights Reserved · Franchino Mold & Engineering