How to Choose the Right Plastic Injection Molding Die?
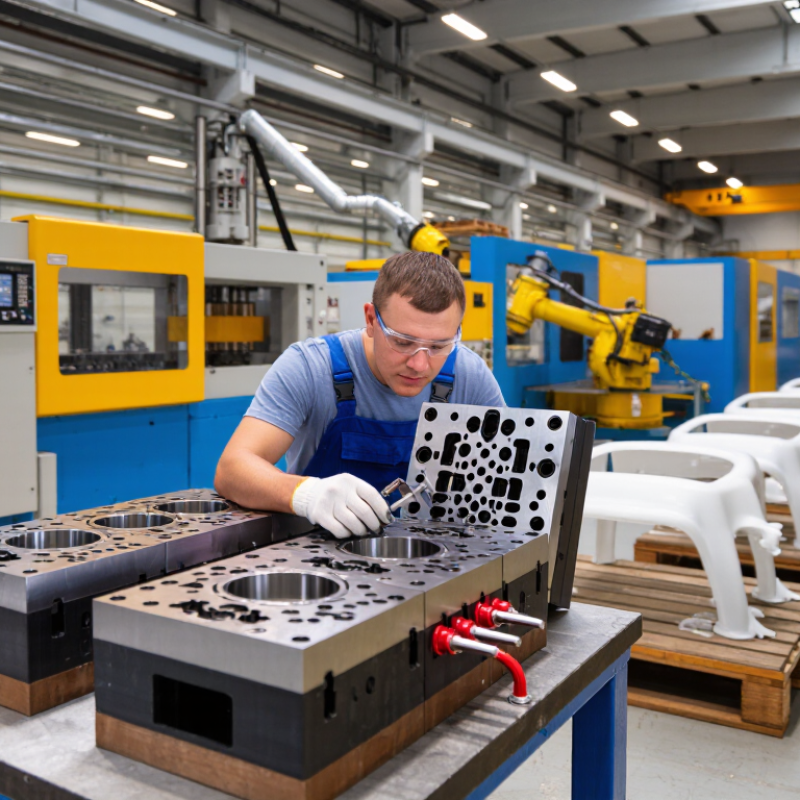
Choosing the right plastic injection molding die affects product quality, cycle time, maintenance, and total production cost. The decision begins with resin behavior, part geometry, annual volume, and dimensional tolerance. A thin-walled medical component needs different cooling and venting than a thick automotive housing. Small details matter.
Industry data supports careful planning. Grand View Research identifies rising demand for injection-molded components across automotive, electronics, packaging, and healthcare applications. Its market analysis also highlights automation, lightweighting, and complex part design as important growth drivers. The Plastics Industry Association’s Size and Impact report shows that plastics manufacturing remains a major economic sector in the United States, supporting more than one million jobs and hundreds of billions of dollars in shipments. These figures suggest strong demand, but they do not make every die investment sensible.
John Bozzelli, an injection molding consultant and founder of Injection Mold Consulting, has stated, “The mold is the heart of the process.” That principle remains practical on the factory floor. A poorly balanced runner system can leave one cavity full while another shows short shots. Inadequate cooling can turn a ten-second cycle into a costly delay. Mold steel, cavity layout, gate design, ejection, and surface finish deserve equal attention.
There is no perfect selection.
A reliable evaluation should compare tool life, repair access, cooling performance, and expected production volume. It should also include resin shrinkage and future design changes. Engineers can use simulation, but simulation is not reality. Results still depend on workmanship, machine settings, and operator experience. This guide examines those choices clearly, while acknowledging one uncomfortable truth: early assumptions are often wrong.
Define Part Requirements: Material Shrinkage, Tolerance, and Annual Volume
Before choosing an injection molding die, define the part’s real requirements. Material shrinkage is not a fixed number. It changes with resin grade, wall thickness, flow direction, cooling, and packing pressure. A 0.5% estimate may look harmless, but it can shift a 100 mm dimension by 0.5 mm. That difference may exceed the assembly limit.
Record critical dimensions, allowable tolerances, and noncritical surfaces separately. For example, a sealing diameter may require ±0.03 mm, while an outer cover may accept ±0.15 mm. Avoid applying tight tolerances everywhere. It increases machining time and can reduce production stability. I once reviewed a part with excellent drawings but uneven ribs. The tool met the nominal dimensions, yet the molded part warped after cooling. The design needed more attention.
Annual volume also shapes the die specification. A few thousand parts may suit a simpler cavity layout and moderate tool steel. Hundreds of thousands of parts require stronger steel, replaceable wear components, reliable cooling, and easier maintenance access. Cycle time matters too. A two-second saving can create major annual capacity. Still, projected volume is often optimistic. Check current orders, growth assumptions, and likely design changes before adding expensive features. Measure real samples during trials, then adjust the die based on data rather than confidence alone.
How to Choose the Right Plastic Injection Molding Die? — Define Part Requirements: Material Shrinkage, Tolerance, and Annual Volume
| Requirement | Typical planning reference | What to define | Implication for die selection and design |
|---|---|---|---|
| Material: ABS | Typical linear molding shrinkage: about 0.4–0.7% | Exact resin grade, colorants, additives, and whether the material is reinforced | Use the selected grade’s data and mold-flow or trial results to establish cavity dimensions; shrinkage varies with part geometry and processing conditions. |
| Material: Polypropylene (PP) | Typical linear molding shrinkage: about 1.0–2.5% | Homopolymer or copolymer grade, filler content, and expected operating temperature | Allow for relatively high and grade-dependent shrinkage. Check warpage and dimensional stability, particularly for large, flat, or unevenly thick parts. |
| Material: Polycarbonate (PC) | Typical linear molding shrinkage: about 0.5–0.7% | Optical or structural requirements, resin grade, and any reinforcement | Specify surface finish and dimensional targets early. Gate location, cooling balance, and residual stress can affect appearance and part performance. |
| Material: Unfilled nylon (PA6) | Typical linear molding shrinkage: about 0.7–1.5%; moisture absorption can also change dimensions | Nylon type, conditioning state, humidity exposure, and critical measurement conditions | Define whether dimensions apply to parts as molded or conditioned. Account for moisture-related dimensional change when setting tolerances. |
| Material: Glass-filled nylon | Shrinkage is generally lower than for the corresponding unfilled grade, but varies by grade and fiber orientation | Glass-fiber percentage, flow direction, and locations of critical dimensions | Evaluate anisotropic shrinkage and warpage. Gate placement and flow direction can cause different dimensions parallel and perpendicular to the fibers. |
| General dimensional tolerance | A preliminary target might be around ±0.10–0.20 mm for a 100 mm feature, subject to part and process capability | Identify critical dimensions, datum scheme, measurement method, and acceptable variation | Do not apply a single tight tolerance to every feature. Tighter tolerances can require more precise tooling, process control, inspection, and validation. |
| Annual volume: prototype / low volume | Typically hundreds to a few thousand parts per year; confirm the actual forecast and part life | Expected lifetime quantity, design-change likelihood, and acceptable cycle time | A simpler tool may be suitable when production demand and tool life are modest. Consider replaceable inserts if design changes are likely. |
| Annual volume: medium volume | Often several thousand to tens of thousands of parts per year, depending on the application | Demand variability, required delivery rate, maintenance access, and planned tool life | Balance initial tooling cost against cycle time, cavity count, wear resistance, and maintenance needs. |
| Annual volume: high volume | Often tens of thousands to hundreds of thousands or more parts per year | Peak production rate, total lifetime quantity, acceptable downtime, and quality targets | Evaluate multi-cavity tooling, automated part removal, robust cooling, wear-resistant components, and planned preventive maintenance. |
| Production and validation plan | Validate dimensions using parts molded with the intended material, machine settings, and measurement conditions | Sampling plan, acceptable variation, process window, and approval criteria | Confirm shrinkage and tolerance capability through mold trials. Published shrinkage figures are starting points, not guaranteed final-part values. |
Note: Shrinkage and tolerance figures are indicative planning ranges. Actual results depend on the specific resin grade, part geometry, wall thickness, mold design, processing conditions, and measurement state; verify them with the material supplier and molding trials.
Related Posts
-
Why Choose Injection Tooling for Global Sourcing?
-
Why Choose a Plastic Mold for Global Manufacturing?
-
Challenges Faced in Injection Tooling Manufacturing Process
-
What is a Plastic Injection Molding Die and How Does It Work?
-

How to Optimize Your Die Mold Production Process for Maximum Efficiency
-
How to Choose the Right Plastic Mold for Your Needs?